What Is the Best Hole Saw for Metal?
Choosing the best Hole Saw For Metal is not a brand-only decision. The right cup depends on the material, thickness, hole diameter, and drill setup. A saw that cuts cleanly through thin sheet may struggle with stainless steel or a thick steel plate. Tooth material matters, too: bi-metal models suit many general jobs, while carbide-tooth designs can be useful for tougher materials. Check the manufacturer’s stated limits before cutting.
The scale of metalworking helps explain why this choice matters. World Steel Association’s World Steel in Figures 2024 reports 1,892.2 million tonnes of crude steel production worldwide in 2023. That figure does not identify a “best” hole saw, but it shows how varied steelworking needs can be. The U.S. Bureau of Labor Statistics’ Survey of Occupational Injuries and Illnesses also tracks workplace injuries by industry, reinforcing that tool selection should go hand in hand with safe work practices. Secure the workpiece, use suitable eye protection, and follow the drill and hole-saw instructions.
Small details count. Slow, controlled pressure and cutting fluid, when recommended, can help manage heat and extend cutter life. Yet no single model performs best in every shop; that is easy to overlook when comparing product claims. This guide weighs cutting material, durability, speed, and value, then explains which features fit common metal-cutting tasks. The goal is a practical choice, not a perfect-sounding promise.
What a Hole Saw for Metal Is and How It Works
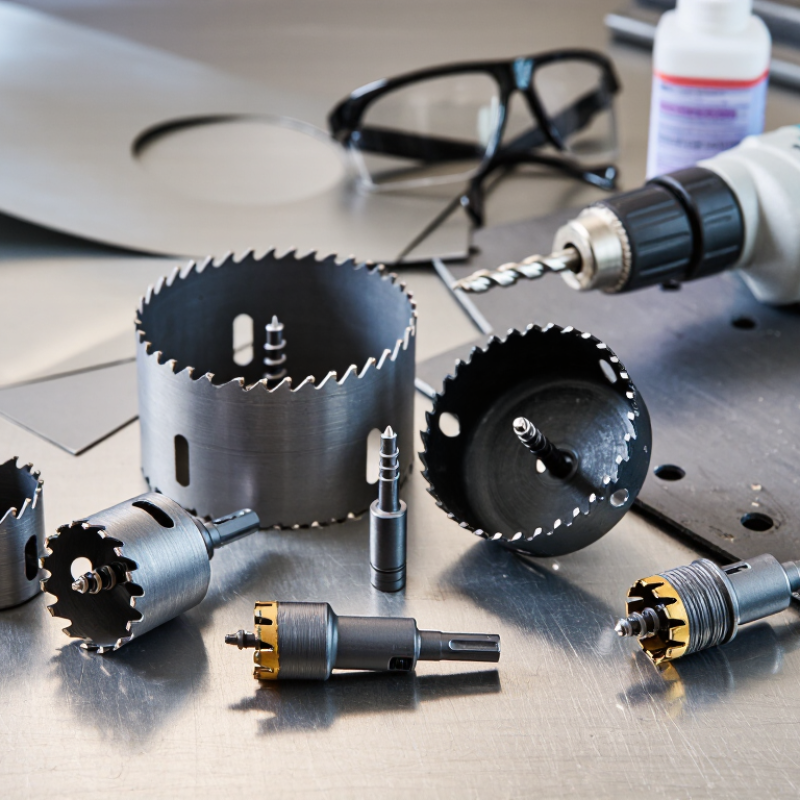
A hole saw for metal is a cup-shaped cutting tool with teeth around its rim. Unlike a twist drill, it cuts a circular groove and leaves a solid metal plug, called a slug. A pilot drill in the center helps guide the saw and reduces wandering as the cut begins.
The saw attaches to an arbor, which connects it to a drill or other compatible machine. As it rotates, the toothed rim cuts around the hole’s edge. Cutting fluid can reduce heat and friction, especially in thicker stock. Keep the workpiece firmly clamped, use eye protection, and follow the tool maker’s speed guidance. Metal chips get hot. Keep hands clear.
The best choice depends on the metal, its thickness, and the hole diameter. A saw suited to thin sheet may struggle in a thick plate, while overly fast cutting can dull teeth or discolor the work. Check that the cutting depth can pass through the material, and clear chips when needed. It sounds straightforward. In practice, setup matters more than expected; even a small wobble can leave a rough, uneven edge.
Key Factors That Determine Metal-Cutting Performance
A hole saw’s performance on metal depends on more than tooth material. For mild steel, a bi-metal saw with hardened teeth is often a practical choice. Cobalt-enriched teeth can tolerate heat better during repeated cuts. For stainless steel or thicker stock, a carbide-tooth model may cut longer, but it needs a stable setup. Tougher teeth are not automatically better.
Tooth pitch matters. Fine, closely spaced teeth usually engage thin sheet more smoothly, while coarser teeth can clear chips from thicker material. A variable pitch may reduce chatter, though it cannot fix a loose workpiece. Keep the metal clamped firmly. Small details matter. A rigid arbor, sharp pilot bit, and steady feed help the saw track cleanly. Use cutting fluid suited to the material, and clear chips when needed. Excessive pressure can overheat teeth or distort thin sheet.
Speed should match the saw diameter and metal type; larger saws generally need slower rotation. Follow the cutter’s speed guidance when available, since one setting does not suit every job. Watch for blue chips, squealing, or a slowing motor. These can signal excess heat or feed pressure. There is no perfect hole saw for every metal. A modest, controlled cut often beats forcing a premium cutter through the work. I would still test on scrap when the finish or fit matters.
Hole Saw Materials, Tooth Designs, and Their Best Uses
What Is the Best Hole Saw for Metal?
Hole Saw Materials, Tooth Designs, and Their Best Uses
For general steel work, a bi-metal hole saw is a practical starting point. Its high-speed-steel cutting rim is joined to a tougher backing, helping resist tooth breakage. Cobalt-bearing M42 steel can retain hardness under heat. ASTM A600 specifies about 8% cobalt for this tool-steel grade. That alloying helps, but it cannot rescue a dull or overheated saw. Use steady pressure and cutting fluid. Small detail, big difference. Fine teeth tend to snag less on thin sheet; thicker stock may suit coarser or variable-pitch teeth, which help clear chips and reduce chatter. The right pitch still depends on the material and saw diameter.
Carbide-tipped saws can suit abrasive metals and repeated production cuts, but their cutting edges are brittle under vibration. Clamp the work securely and avoid forcing the cut. ISO 513:2012 divides hardmetal cutting tools into application groups such as P, M, and K—a reminder that “carbide” does not mean one universal grade. Stainless steel needs careful heat control and lubrication. Aluminum needs sharp teeth and chip clearance to prevent chips packing into the gullets. Not always. A clean edge is not guaranteed. Tooth wear, alloy, and sheet thickness all affect the result, so a test cut on scrap is worthwhile when the material is unfamiliar. It feels cautious, perhaps overly so, but it can prevent a chipped tooth or ruined workpiece.
What Is the Best Hole Saw for Metal?
Typical suitability by hole-saw tooth design and workpiece material
How to read this chart: Ratings are practical guidance, not standardized test results (1 = generally unsuitable; 5 = a strong typical choice). Bi-metal hole saws are versatile for common sheet metals; carbide-tipped designs are often preferred for tougher materials such as stainless steel and cast iron. Check the tool’s specifications, use suitable cutting lubricant, and follow the recommended speed and feed.
How to Choose a Hole Saw for Your Metalworking Task
What Is the Best Hole Saw for Metal?
How to Choose a Hole Saw for Your Metalworking Task
Start with the workpiece, not the tool. Thin mild-steel sheet usually suits a bi-metal hole saw with fine, variable-pitch teeth. For stainless steel or repeated heavy cuts, a carbide-tipped model may last longer, though it costs more. Check the saw’s cutting depth against the material thickness, and confirm that its arbor fits your drill. A large diameter needs slower rotation than a small one. Keep it steady.
Metal labels can hide big differences. World Steel Association’s World Steel in Figures 2024 reports 1,892.2 million tonnes of crude steel production in 2023. That figure reflects the scale of steel use, not the hardness of your specific workpiece. Identify the alloy where possible, then follow the hole-saw maker’s speed guidance for that material and diameter. Clamp the sheet firmly, mark the center, and use cutting fluid when recommended. Clear chips before they pack into the teeth. I still find feed pressure easy to misjudge: pushing harder can make the cut hotter, not faster. Stop if the saw chatters, overheats, or binds, and inspect the teeth before continuing.
How to Use and Maintain a Metal-Cutting Hole Saw
What Is the Best Hole Saw for Metal?
How to Use and Maintain a Metal-Cutting Hole Saw
A suitable metal-cutting hole saw has teeth designed for the material and a diameter that matches the opening you need. Check its stated material range before use; a saw intended for thin sheet may not suit thick steel. Secure the workpiece firmly, mark the center, and use a pilot bit to keep the cut on track. Wear eye protection, and clamp loose sheet metal rather than holding it by hand. Small movements matter.
Set the drill to a low speed appropriate for the saw and metal, following the tool maker’s guidance. Apply cutting fluid when recommended, then use steady pressure without forcing the teeth. If the saw starts to chatter, stop and check the setup. Chips can pack into the teeth, so clear them only after the drill is off and the saw has stopped. Let it cool. I’ve seen rushed cuts leave rough edges and overheated teeth; slowing down is less exciting, but usually kinder to the tool. Afterward, brush away chips, wipe the saw dry, and inspect for missing or dulled teeth. Store it dry, with a light rust-preventive coating if needed. Replace a damaged saw rather than trying to sharpen teeth that are not designed for sharpening.